The Cauvery is the lifeline of Trichy, Thanjavur, Tiruvarur and Nagapattinam. It supplies drinking water to lakhs of homes and irrigates the rice bowl of Tamil Nadu. Industries that sit in this basin, from sugar mills and distilleries to chemical, pharma and food units, are therefore watched closely by the pollution control board, and many must operate with zero liquid discharge. Intellect Aqua plans, builds and runs ZLD plants for industries across Trichy and the delta, with designs based on each unit's own effluent rather than a standard package.
Is ZLD Mandatory for Your Unit?
Start with your consent order from the Tamil Nadu Pollution Control Board. If it says no effluent may leave the premises, ZLD is not optional. Even where discharge is allowed, many delta units choose high water recovery because:
- Groundwater is saline in parts of the delta and fresh water is costly
- Canal and river supply depends on monsoon and upstream releases
- Buyers and lenders increasingly ask about water stewardship
We help you read the consent conditions and decide whether you need full ZLD now, or high recovery first with ZLD added later.
Distillery and Sugar Mill Effluent
Sugar mills and molasses-based distilleries in the region produce some of the strongest effluent in any industry. Distillery spent wash is dark brown, acidic and extremely high in organic load. It cannot go straight to RO. The usual route is:
- Anaerobic digestion to cut organic load and produce biogas for the boiler
- Concentration of the treated spent wash in a multiple effect evaporator
- Co-processing or incineration of the concentrate, such as burning in a boiler, where approvals allow
- Polishing of condensate through RO so it can be reused in fermentation, cooling or the boiler
Sugar mill process water, condenser cooling water and floor washings are lighter and are usually treated with a conventional ETP, filtration and RO. See distillery wastewater treatment.
Chemical, Pharma and Food Units
These units produce smaller volumes, but the composition changes from batch to batch. We provide large equalisation tanks, careful pH control, and sometimes oxidation to break down compounds that resist biological treatment. After that, the effluent goes through ultrafiltration, two- or three-stage RO and an evaporator for the final reject. Food and dairy units nearby benefit most from recovering their wash water. The full front-end treatment is explained on our Trichy ETP page.
Choosing the Evaporator: MEE or MVR?
| Factor | Multiple effect evaporator (MEE) | Mechanical vapour recompression (MVR) |
|---|---|---|
| Energy source | Steam | Electricity |
| Best for | Sugar mills and distilleries with their own boilers or cogeneration | Units without spare steam |
| Capital cost | Lower | Higher |
| Running cost | Low when steam is cheap | Low when power is affordable |
For many delta sugar complexes, spare exhaust steam makes MEE the natural choice. A chemical unit buying grid power and no steam may find MVR cheaper over ten years. We work out both before recommending one.
What Makes a ZLD Plant Fail in Practice
Most ZLD complaints we hear come down to a few causes:
- The evaporator was sized on brochure numbers, not actual reject volume
- RO membranes foul because pre-treatment was skipped to save money
- Antiscalant dosing stops when the drum runs out
- Nobody records recovery, so slow decline goes unnoticed
- Seasonal changes, such as crushing season in sugar mills, were never planned for
Our designs start from a measured mass balance for peak season. Every critical dosing point gets a level alarm, and operators get a simple daily sheet that shows when recovery starts to slip.
Phased ZLD for Growing Units
Not every unit can fund a full ZLD plant in one go. A practical path is:
- Fix the ETP so treated quality is stable
- Add UF and RO to recover 60–75% of the water for reuse
- Add the evaporator once the RO reject volume is known and steady
Each phase pays for itself through water savings and lower tanker purchases. Each also builds the operating data that makes the next phase cheaper to design.
Turning Around an Existing Plant
If your ZLD plant has never reached its rated recovery, we begin with a walk-through and sampling at every stage. We then compare actual flows with the original design. The fix is often smaller than expected: better clarification, a corrected antiscalant, or a cleaning schedule. Where equipment really is undersized, we show you the numbers before suggesting anything new.
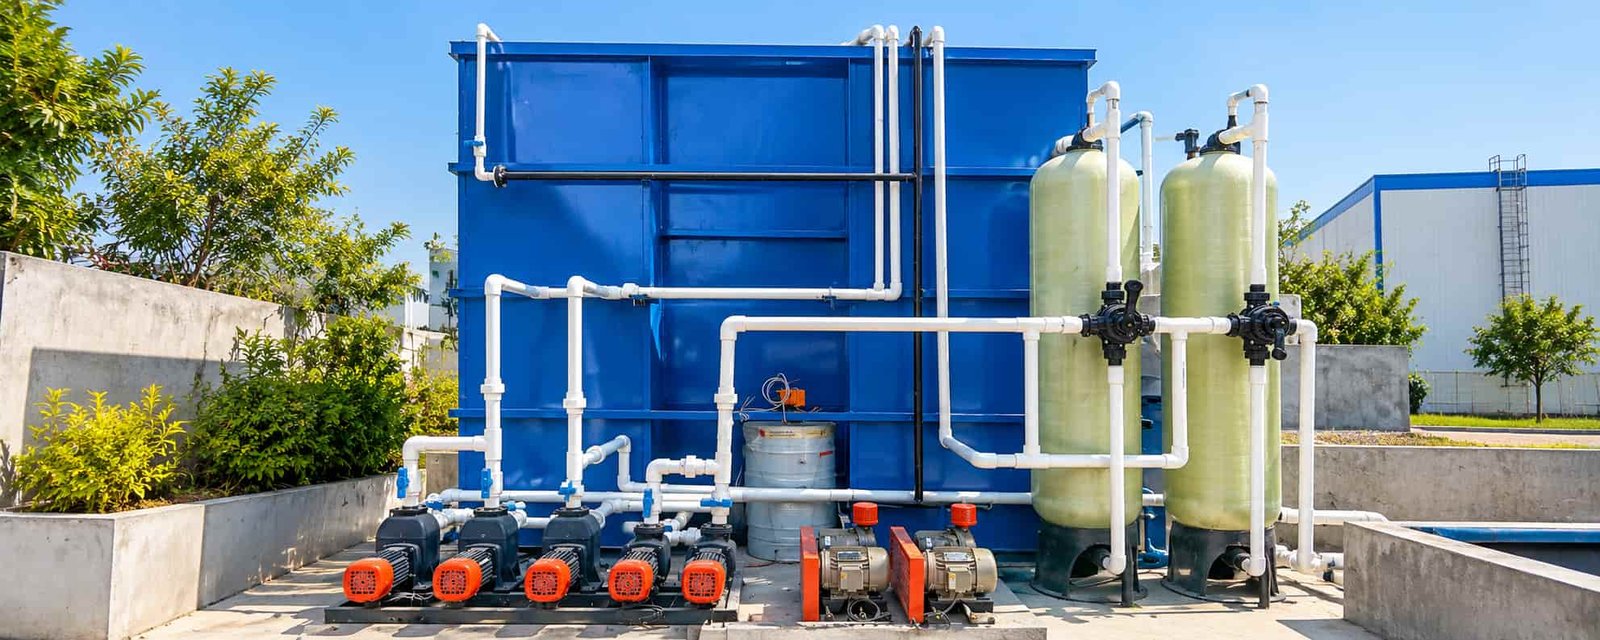
Operating Support
Many delta units find it hard to keep skilled evaporator and RO operators. We offer operation contracts with trained staff, chemical supply, membrane cleaning and monthly performance reports. Shorter visit-based AMC plans are available for plants with in-house operators.
Why Delta Industries Work With Us
- Designs built on your measured effluent and peak-season flows
- MEE and MVR compared honestly on your own steam and power costs
- ETP, RO and evaporator from one team, so there is no blame game between vendors
- 4.9★ from 53 Google reviews, 700+ projects and 15+ years of industry experience
Intellect Aqua is a Coimbatore-based water and wastewater treatment company that builds and services plants across Tamil Nadu, including Trichy.
Where We Work
Trichy city, Thuvakudi, Thiruverumbur, Manapparai, Lalgudi, Musiri, Srirangam, Perambalur, Ariyalur, Pudukkottai, Thanjavur, Kumbakonam, Tiruvarur and Nagapattinam.
ZLD plants are also built for units in Madurai, Karur, Salem and Chennai.
Talk to a ZLD Engineer
Send us your consent order, daily effluent volume and a recent lab report. We will tell you within a week what a realistic ZLD scheme for your unit looks like.